Family Molds and Multi-Cavity Molds for a Lower Price per Part
A multi-cavity mold makes 2, 4 or 8 copies of one part in every shot. A family mold makes the different parts of one product together. Either way you get more parts per cycle, a lower price per part, and parts that match in color and material.
Compare all molding methods- Cavities per mold
- 1 to 8
- Different parts in one shot
- Family
- Standard tolerance
- ±0.10 mm
- Presses, about
- 50 to 500 t
How Family and Multi-Cavity Molds Work
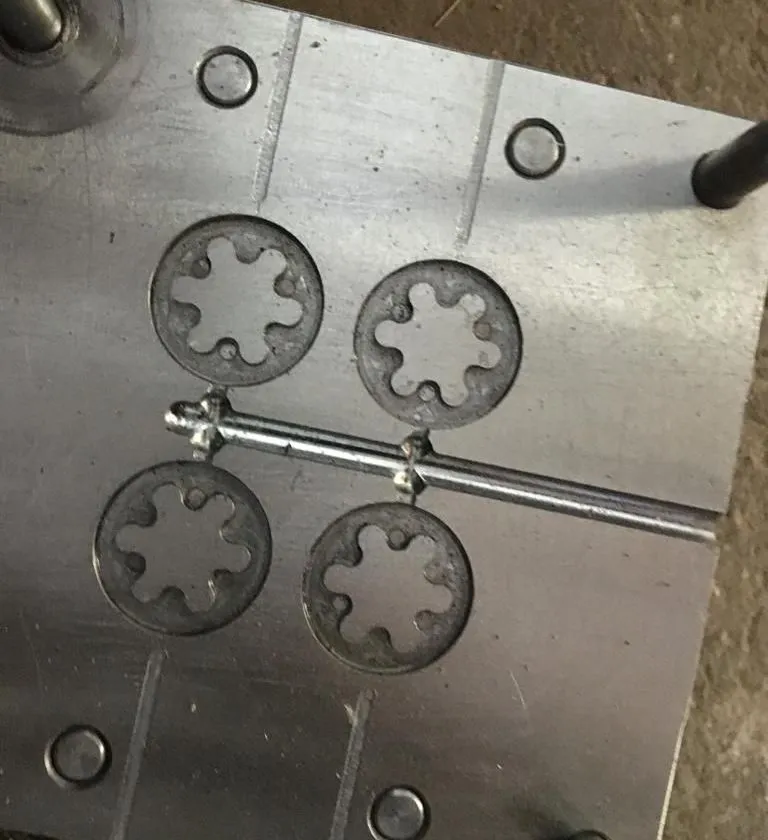
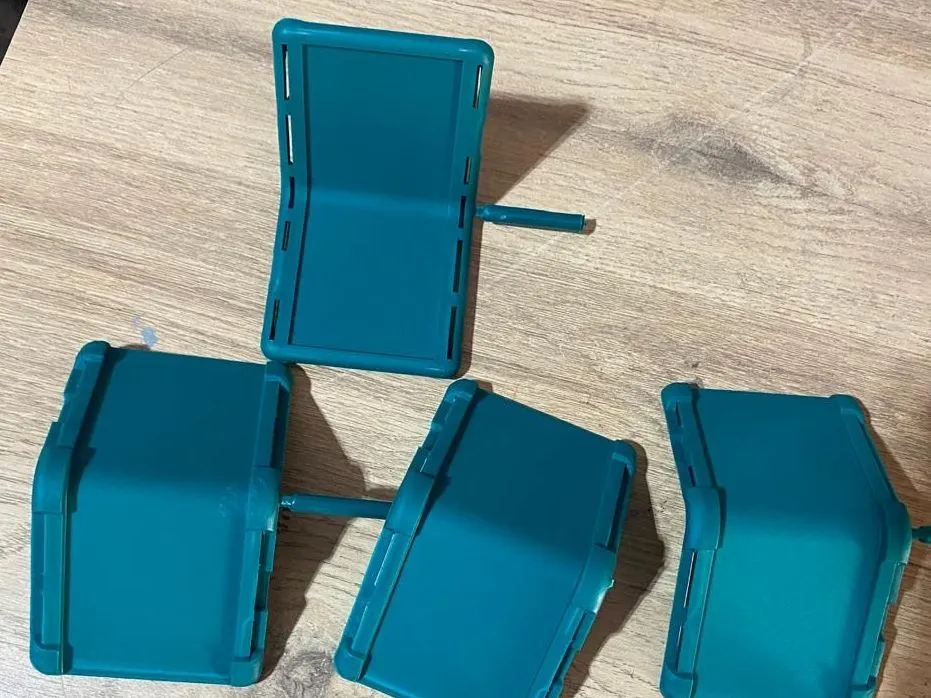
The melt enters the mold at one sprue and splits along runners into every cavity. The runners are sized so each cavity fills at the same moment, so every part in the shot comes out the same. Then the mold opens and all of them are ejected together.
- 01
Volume and part review
We look at your yearly quantity, part size and press size to choose the number of cavities.
- 02
Cavity layout and runners
Cavities are placed and runners balanced so every cavity fills and packs the same.
- 03
Mold build
The mold is machined in-house with matching cavities and cooling for each one. Cavity numbers can be cut in for traceability.
- 04
First shots from every cavity
Parts from each cavity are checked. You approve samples on video, then in hand, before production.
- 05
Production and checks
Every shot gives several parts, checked against your drawing, then packed and shipped.
Is a Multi-Cavity or Family Mold Right for You?
More cavities cost more up front and save on every part after. Here is what we build, and when a simpler mold is the better buy.
Typical multi-cavity figures
- Cavities
- 1, 2, 4 or 8, or a family mold
- Tolerance
- ±0.10 to ±0.20 mm
- Presses
- About 50 to 500 tonnes
- Mold types
- Aluminum or steel, by volume
- Best-fit quantity
- Higher yearly volumes, or parts that ship as a set
- First samples
- 4 to 8 weeks after design sign-off
Typical values. Your quote recommends the number of cavities for your part and volume.
Choose a multi-cavity or family mold when you need
- Thousands of small parts a year
- A lower price per part at volume
- Several parts of one product that ship together
- Matching color across a set of parts
- Shorter production runs for the same quantity
- Caps, clips, buttons and other small parts
Consider instead
- Single-cavity plastic moldingFor large parts or while demand is still uncertain.Plastic molding
- Injection mold toolingFor choosing the mold steel and an aluminum bridge mold.Mold tooling
- OvermoldingFor two materials joined in one part instead of a set.Overmolding
- Vacuum castingFor 10 to 25 sets of parts before any metal mold.Vacuum casting
How Many Cavities Should Your Mold Have?
The right number depends on part size, yearly volume and the press. Here is how the options trade mold cost against the price per part.
Single cavity
1 part per shot
The simplest and lowest-cost mold, and the easiest to change while the design settles.
- Mold cost
- Lowest
- Price per part
- Highest
Ideal forLarge parts, launches, uncertain demand
2 cavities
2 identical parts per shot
Doubles the output per cycle for a moderate step up in mold cost.
- Mold cost
- Moderate
- Price per part
- Lower
Ideal forMedium volumes, medium-size parts
4 cavities
4 identical parts per shot
A common choice for small parts once demand is steady.
- Mold cost
- Higher
- Price per part
- Low
Ideal forSmall parts at steady volume
8 cavities
8 identical parts per shot
For small parts in large numbers, where cycle time drives the cost.
- Mold cost
- Highest
- Price per part
- Lowest
Ideal forCaps, clips, buttons at high volume
Family mold
Different parts per shot
Molds the parts of one product together, in the same material and color.
- Mold cost
- Less than separate molds
- Price per set
- Lower
Ideal forMulti-part products of similar size
Multi-cavity family
Several sets per shot
Two or more full sets of a product’s parts in every shot, for products selling at volume.
- Mold cost
- High
- Price per set
- Lowest
Ideal forSmall multi-part products at volume
General guidance. Your quote recommends a layout for your part and volume.
Family Mold or Multi-Cavity Mold?
Both put more parts in each shot, but they suit different products. Here is how they compare.
What it makes
- Multi-cavity mold
- 2, 4 or 8 copies of one part
- Family mold
- Different parts of one product
Best when
- Multi-cavity mold
- You need many of the same part
- Family mold
- The parts ship together as a set
Part sizes
- Multi-cavity mold
- All identical
- Family mold
- Similar size and wall thickness work best
Material and color
- Multi-cavity mold
- One material and color
- Family mold
- One material and color for every part in the set
Filling
- Multi-cavity mold
- Naturally balanced
- Family mold
- Runners sized so each different cavity fills evenly
Watch out for
- Multi-cavity mold
- A bigger press and a longer mold build
- Family mold
- Making more of one part than you need
| Compare | Multi-cavity mold | Family mold |
|---|---|---|
| What it makes | 2, 4 or 8 copies of one part | Different parts of one product |
| Best when | You need many of the same part | The parts ship together as a set |
| Part sizes | All identical | Similar size and wall thickness work best |
| Material and color | One material and color | One material and color for every part in the set |
| Filling | Naturally balanced | Runners sized so each different cavity fills evenly |
| Watch out for | A bigger press and a longer mold build | Making more of one part than you need |
General guidance. Your DFM review recommends the layout for your parts.
Family and Multi-Cavity Mold Questions
What is the difference between a family mold and a multi-cavity mold?
A multi-cavity mold makes several copies of the same part in each shot. A family mold makes different parts of one product in each shot, for example a housing and its cover.
How many cavities can a mold have?
We build molds with 1, 2, 4 or 8 cavities, or as a family mold. The right number depends on part size, yearly volume and the press, and we recommend one in your quote.
Do more cavities always lower the cost?
They lower the price per part but raise the mold cost. At low volumes a single-cavity mold is often cheaper in total. Tell us your yearly quantity and we show both ways.
When does a family mold not work well?
When the parts differ a lot in size or wall thickness, need different materials or colors, or are needed in very different quantities. Then separate molds are usually better.
Are parts from different cavities identical?
The runners are balanced so each cavity fills the same, and parts from every cavity are checked at first samples. Cavity numbers can be molded into each part so any part can be traced back to its cavity.
Who owns a multi-cavity mold?
You do, from day one, like every mold we build for you, with a mold passport recording its cavities, steel and shot count.
Trusted By Product Companies Worldwide
Verified reviews from clients in USA, UK, Germany, Australia, Canada and more.
Ready to scale up?
Get More Parts From Every Shot
Send 3D models of your parts and your yearly quantities. An engineer recommends a cavity layout and replies with mold and part prices within 24 hours.


