Overmolding and Insert Molding for Grips, Seals and Molded-In Metal
A soft layer molded onto a rigid part, or a metal insert molded into it, so the product comes out of the mold as one piece. No gluing, fewer assembly steps, and a bond designed in from the first DFM review.
Compare all molding methods- Materials in one molded part
- 2 in 1
- Standard tolerance
- ±0.10 mm
- Plates, magnets, inserts molded in
- Metal
- First samples, typical
- 4 to 8 weeks
How Overmolding and Insert Molding Work
In insert molding, a metal or plastic part is placed in the mold and the plastic is molded around it. In overmolding, a rigid part is molded first and a second, softer material is molded over it. Either way, the product leaves the mold as one part.
- 01
DFM review of both materials
We check the substrate, the soft layer or insert, how they lock together and where the shutoffs sit.
- 02
Material pairing
We choose a soft material that bonds to your rigid plastic, or add mechanical locks where it will not.
- 03
Mold build
The mold is designed to hold the insert or substrate in the same place every shot, then machined in-house.
- 04
Overmolding and first samples
Inserts or substrates are loaded and overmolded. You approve the first samples for bond, coverage and fit.
- 05
Production and checks
Parts are molded and checked for bond, flash and dimensions, then packed and shipped.
Is Overmolding Right for Your Part?
Overmolding saves assembly and gives a part that feels and seals better. Here is what it holds, and when two separate parts make more sense.
Typical overmolding figures
- Tolerance
- ±0.10 to ±0.20 mm
- Soft layer
- TPE, TPU or liquid silicone, about 20 to 95 Shore A
- Rigid part
- ABS, PC, PC/ABS, PP, nylon
- Inserts
- Steel plates, magnets, brass threaded inserts
- Best-fit quantity
- 500 to 100,000+ parts a year
- First samples
- 4 to 8 weeks after design sign-off
Typical values. Your quote confirms the exact figures for your part.
Choose overmolding when you need
- A soft grip on a rigid handle or housing
- A seal molded onto a housing
- Weights or magnets locked inside the part
- Threaded inserts that will not pull out
- Fewer parts and assembly steps
- Two colors or textures in one part
Consider instead
- Plastic injection moldingFor a single rigid material with no soft layer.Plastic molding
- Silicone rubber moldingFor a separate soft part that fits by hand.Silicone molding
- Family moldsFor several separate parts of one product in one shot.Family molds
- Vacuum castingFor prototypes of two-material parts before tooling.Vacuum casting
Overmolding and Insert Molding in Real Products
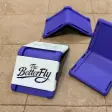
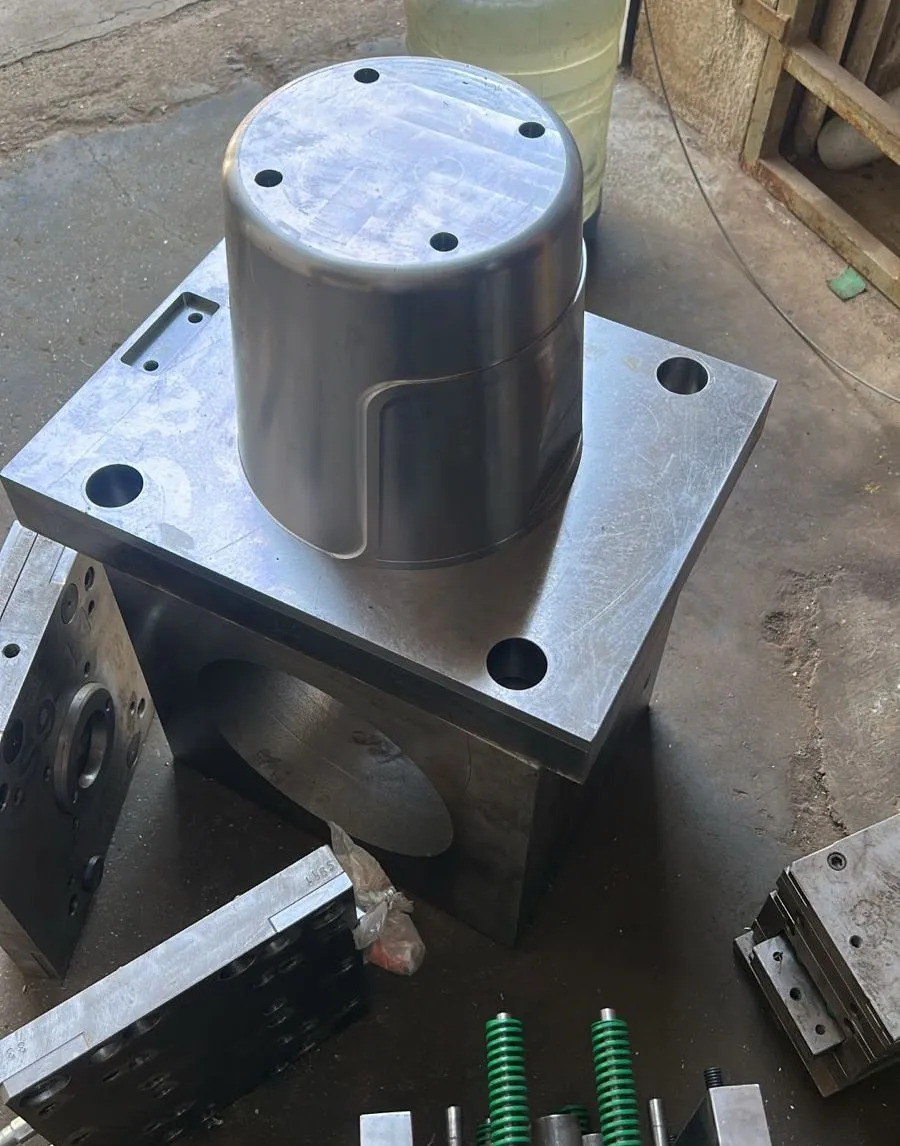
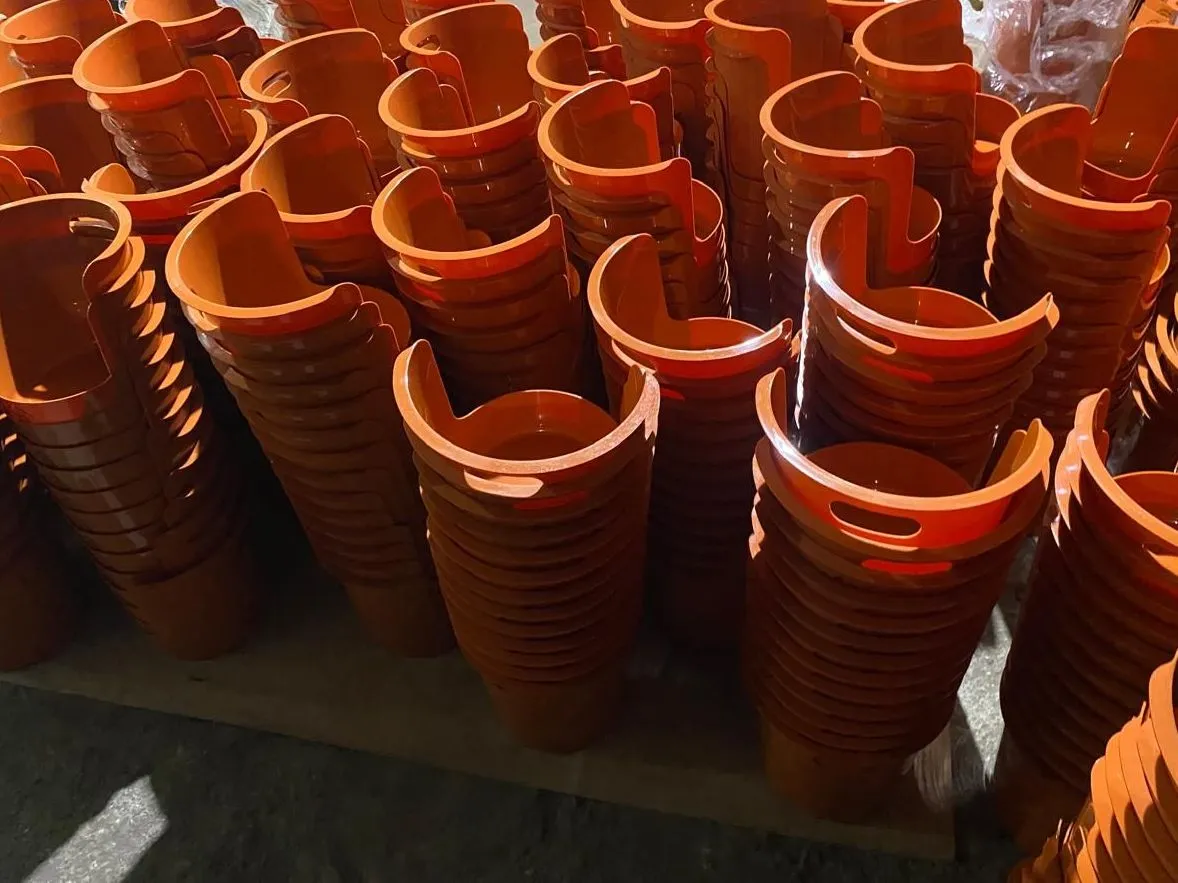
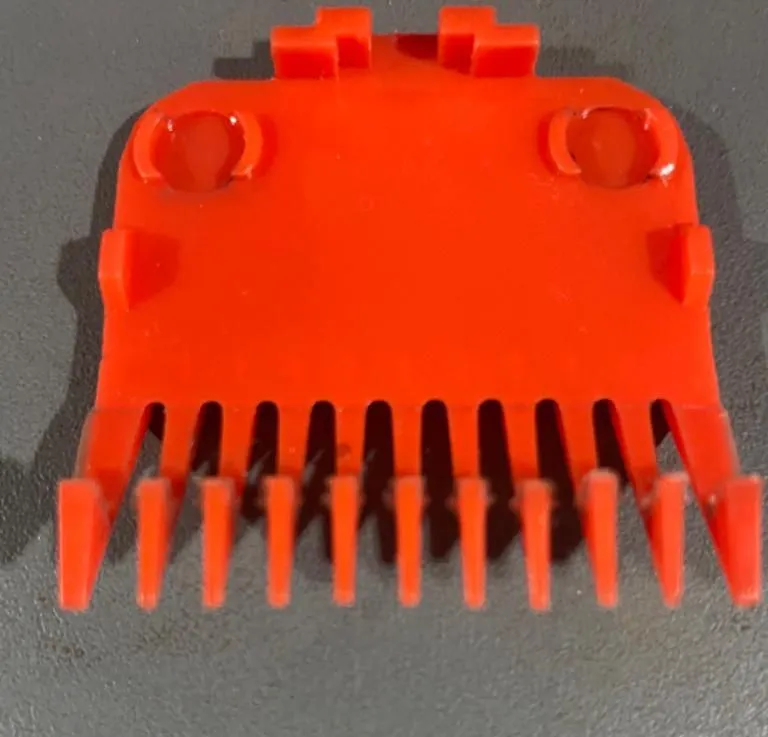
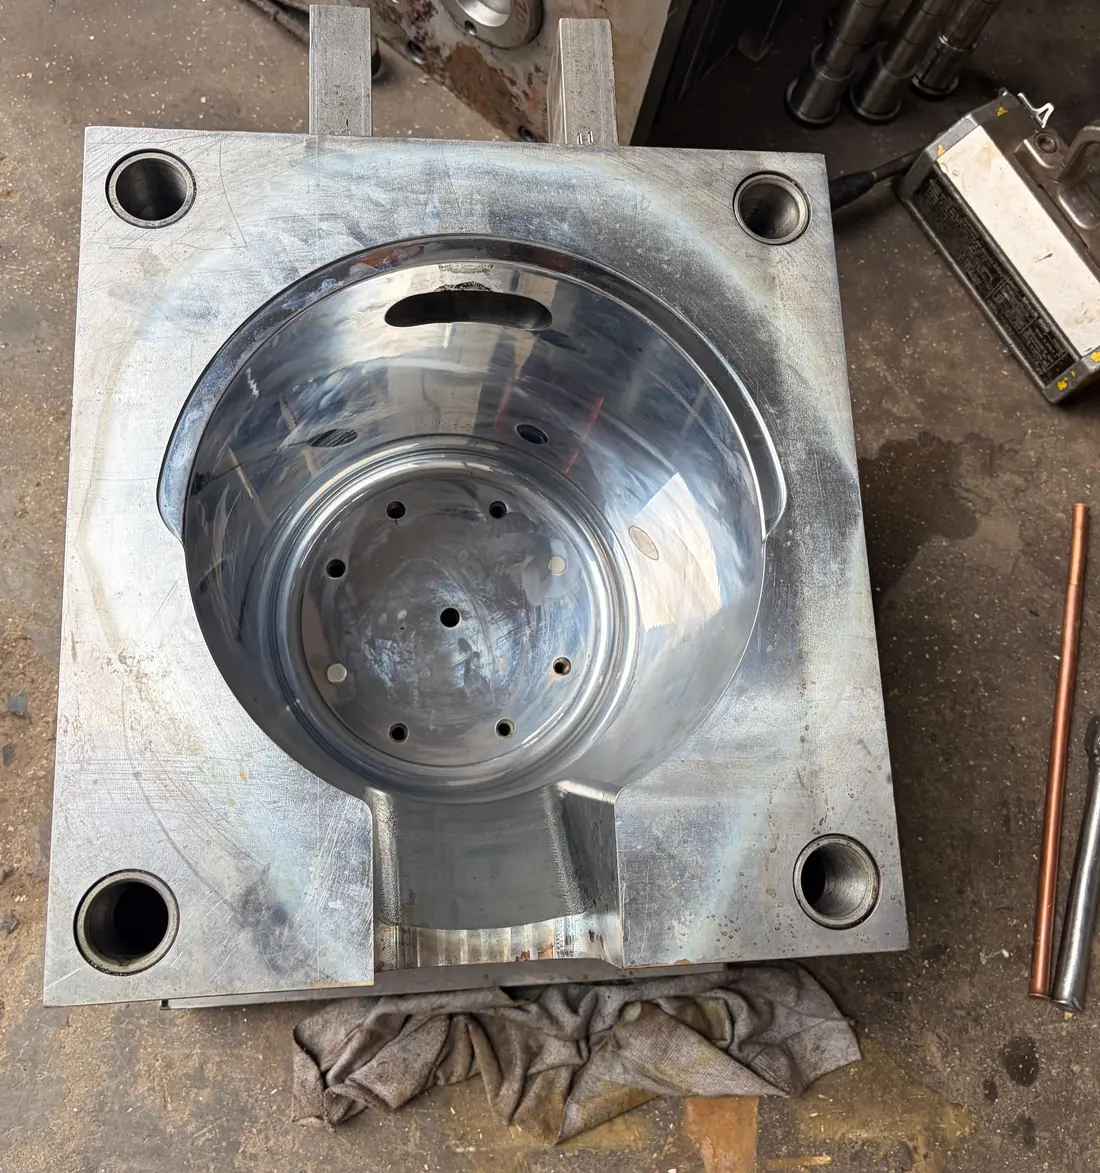
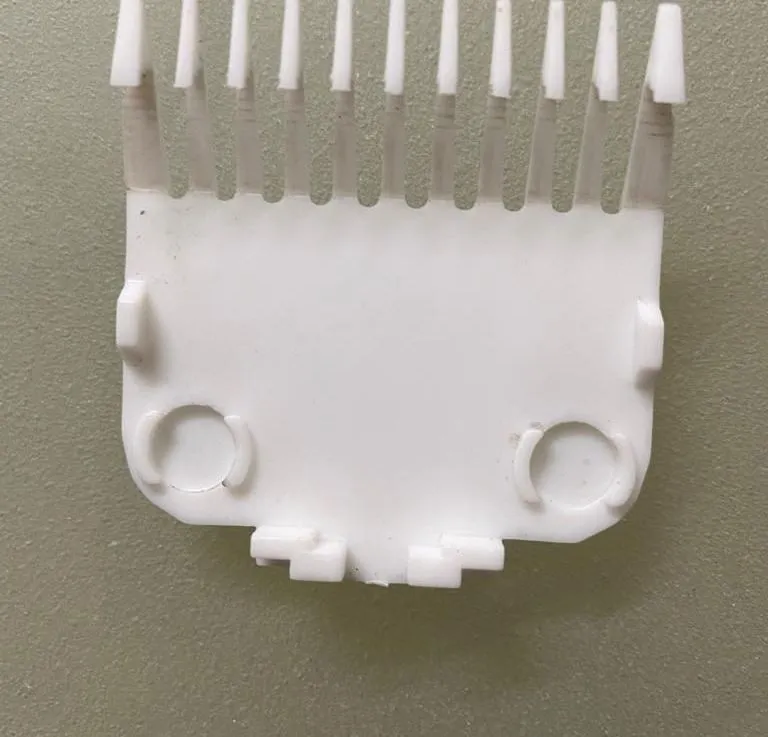
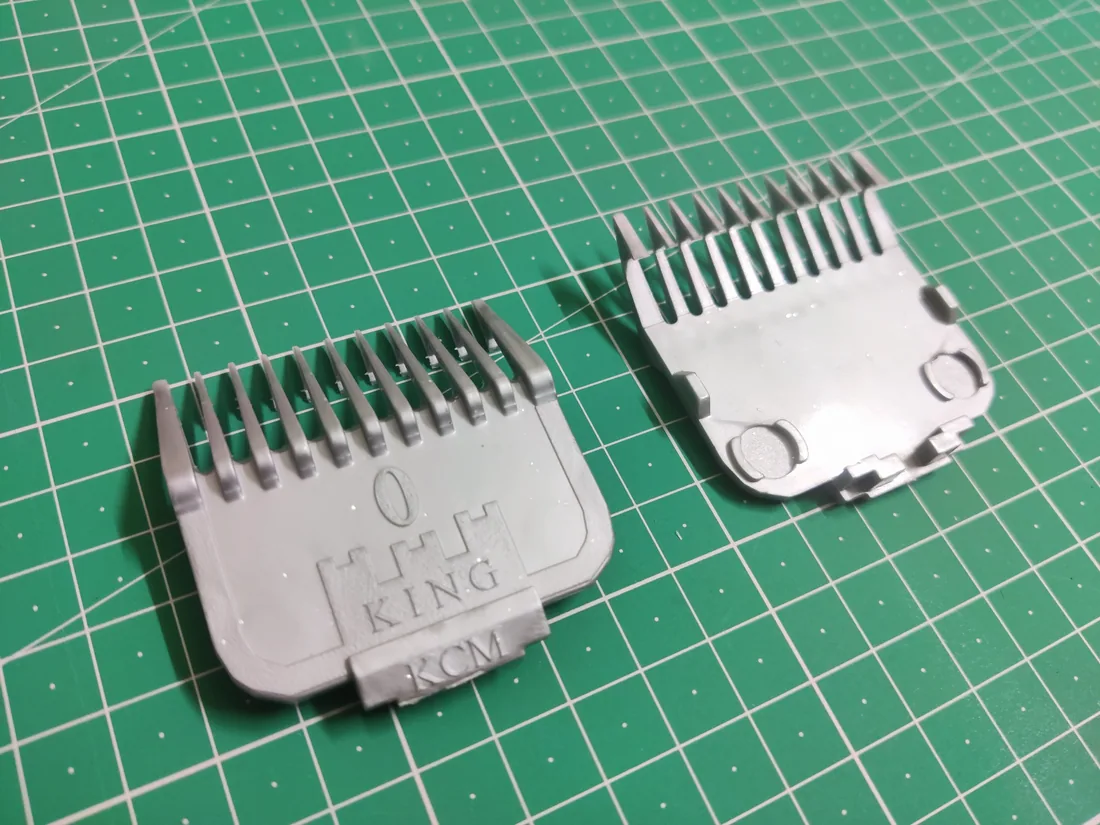
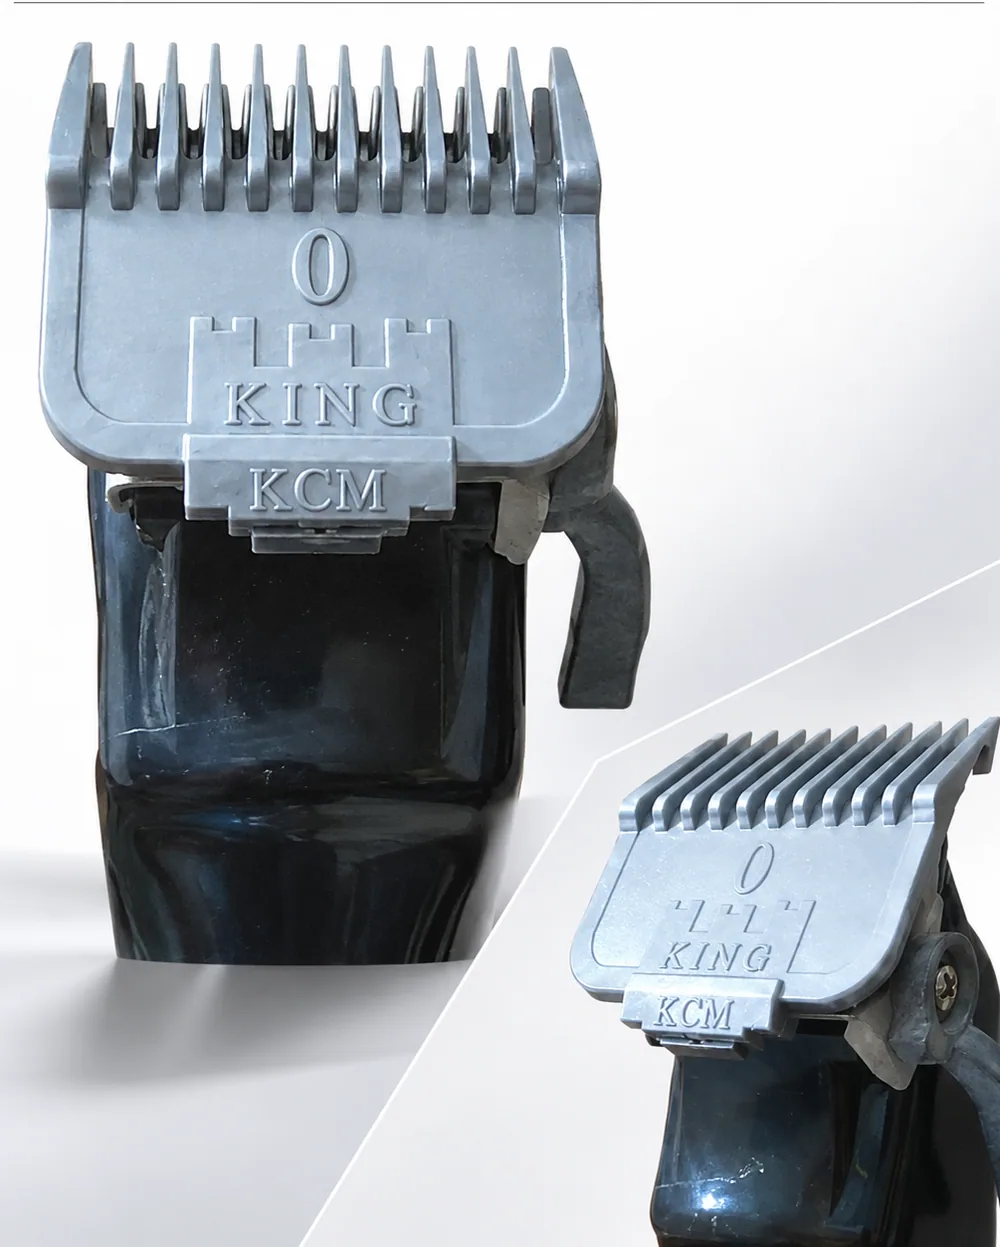
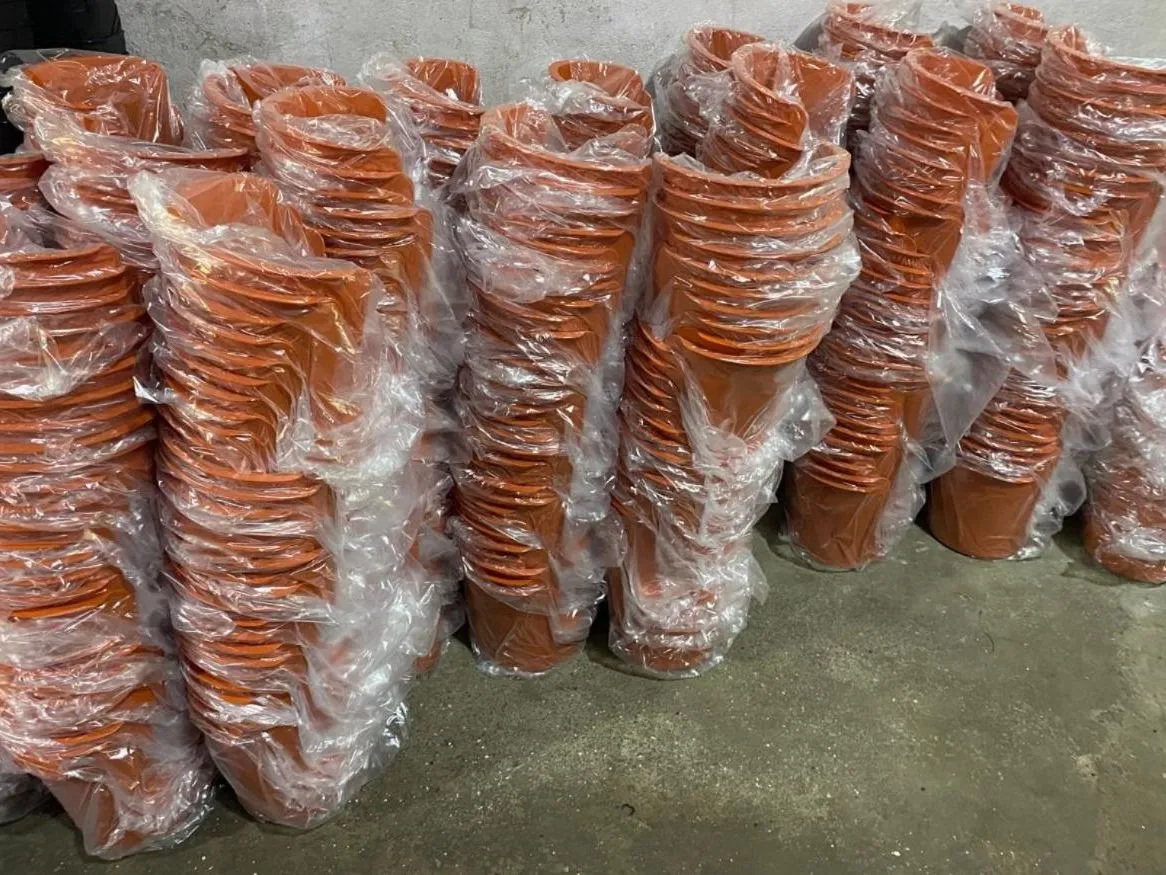
Two client products where something had to be molded into the part: a steel weight in a pet bowl and magnets in clipper guards.
Which Soft Material Should Go On Top?
The soft layer has to bond to the rigid part underneath. Pick by feel and by what the part meets in use, and we confirm the pairing with you.
TPE
Soft-touch elastomer
The most common overmold: a soft, rubbery layer for grip and comfort, in many colors.
- Hardness
- ≈ 20 to 90 Shore A
- Service temp.
- ≈ −40 to 125 °C
- Bonds to
- PP, ABS, PC (grade-matched)
Ideal forGrips, handles, soft buttons
TPU
Tough and abrasion resistant
Harder wearing than TPE, for overmolds that rub, flex or take knocks.
- Hardness
- ≈ 70A to 95A Shore
- Service temp.
- ≈ −40 to 100 °C
- Bonds to
- PC, ABS, PC/ABS
Ideal forBumpers, protective edges, tool grips
Liquid silicone (LSR)
Heat resistant and soft
For soft layers that must take heat or stay flexible in the cold, with self-bonding grades for plastics.
- Hardness
- 10 to 80 Shore A
- Service temp.
- ≈ −50 to 200 °C
- Bonds to
- PC, PBT, nylon (self-bonding grades)
Ideal forSeals, gaskets, skin-contact surfaces
Typical published values. Bonding depends on the exact grades, so we confirm each pairing during DFM.
Overmolding Design Rules
Most overmolding problems come from the joint between the two materials. Design the joint well and the soft layer stays put.
Soft layer thickness
- Recommended
- About 1 to 3 mm, even across the area
- Why it matters
- Thin layers tear, thick ones sink and cost more
Rigid part wall
- Recommended
- At least as thick as the soft layer
- Why it matters
- A thin substrate deforms under the second shot
Mechanical locks
- Recommended
- Through holes, grooves or undercuts under the soft layer
- Why it matters
- Locks hold even where the materials bond poorly
Edges of the soft layer
- Recommended
- End in a groove or step, not on a flat face
- Why it matters
- A clean shutoff stops flash and peeling edges
Inserts
- Recommended
- Locate positively in the mold; knurled or with flats
- Why it matters
- Inserts that move or spin leave flash and loose parts
Material pairing
- Recommended
- Choose grades that bond chemically
- Why it matters
- A wrong pair peels off in use
| Rule | Recommended | Why it matters |
|---|---|---|
| Soft layer thickness | About 1 to 3 mm, even across the area | Thin layers tear, thick ones sink and cost more |
| Rigid part wall | At least as thick as the soft layer | A thin substrate deforms under the second shot |
| Mechanical locks | Through holes, grooves or undercuts under the soft layer | Locks hold even where the materials bond poorly |
| Edges of the soft layer | End in a groove or step, not on a flat face | A clean shutoff stops flash and peeling edges |
| Inserts | Locate positively in the mold; knurled or with flats | Inserts that move or spin leave flash and loose parts |
| Material pairing | Choose grades that bond chemically | A wrong pair peels off in use |
Recommended values. Your DFM review confirms them for your part and material pair.
Overmolding Questions
What is the difference between overmolding and insert molding?
Insert molding places a ready-made part, usually metal, in the mold and molds plastic around it. Overmolding molds a second material, usually a soft one, over a rigid plastic part. Both give one finished part out of the mold.
What can be molded into a plastic part?
Steel plates and weights, magnets, brass threaded inserts and other metal parts. On our Custom Pet Feeder Bowl, a steel plate is overmolded into the base as a dead weight.
Will the soft layer peel off?
Not if the materials are paired and the joint is designed well. We choose grades that bond to each other and add mechanical locks, such as holes or grooves, where they help.
Does overmolding cost more than two separate parts?
The mold costs more, but you save the assembly, glue and the second part handling on every unit. At higher volumes overmolding is often cheaper overall. We can quote both ways.
Can I prototype an overmolded part first?
Yes. Vacuum casting can make prototypes with a rigid and a rubber-like material, so you can test the feel and fit before tooling.
Who owns the overmolding mold?
You do, from day one. Like every mold we build, it has a mold passport and is never used for another client.
Trusted By Product Companies Worldwide
Verified reviews from clients in USA, UK, Germany, Australia, Canada and more.
Two materials, one part?
Get Your Overmolded Parts Made
Send a 3D model with both materials, or the insert. An engineer reviews the joint and replies with mold and part prices within 24 hours.


