Mudgards: Branded, Heavy-Duty Ground Reinforcement Grid for the USA Market
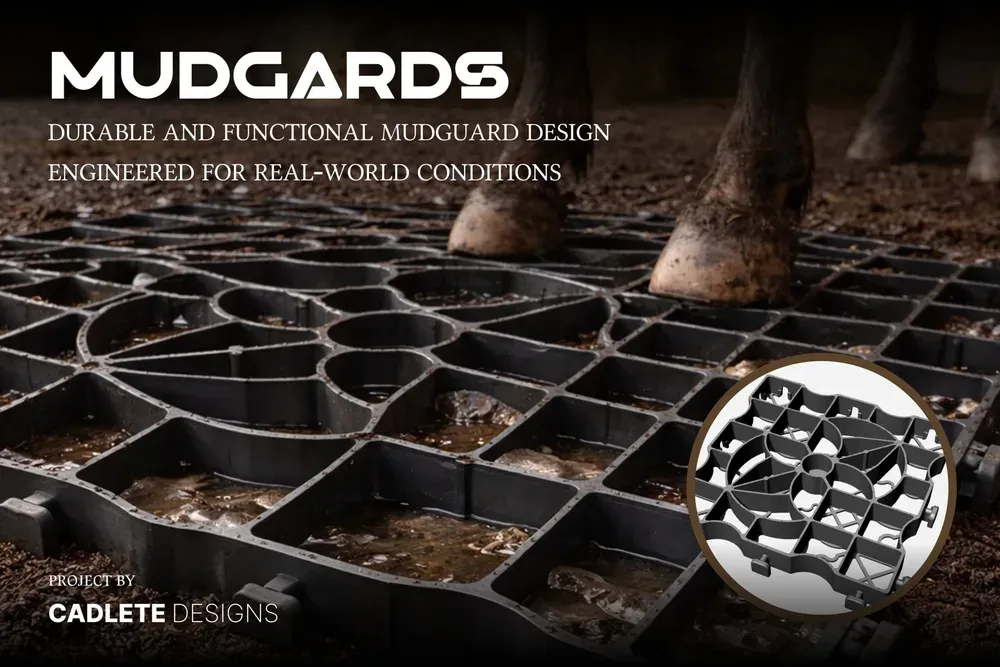
A generic mud grid, rebuilt as a branded product
Our client, a USA company specializing in horse-related infrastructure and supplies, wanted to turn a generic ground reinforcement grid into a custom, branded solution for horse barns, training areas, and outdoor terrain.
The goal went beyond basic function: the grid needed to reflect the client’s brand identity and durability standards while staying interlocking, load-bearing, and cost-effective to mold at volume.
What made this project hard
Brand integration
A design language aligned with the client’s horse-focused brand, without weakening structural efficiency.
Snap-fit engineering
An interlocking mechanism that would not disengage under the weight of vehicles, trucks, and equipment.
Manufacturing at 700 to 800 grams
Large plastic parts needing a precise injection mold for consistent quality run after run.
Zero-undercut design
Keeping tooling cost-effective while integrating complex geometry and snap-fit features.
From generic grid to a heavy-duty branded product
Four stages, one team, no handoffs between them.
Concept Exploration
Over 50 grid pattern concepts explored, incorporating horse-inspired aesthetics.
Snap-Fit Prototyping
3D-printed prototypes validated the interlocking mechanism.
DFM for Molding
Zero-undercut geometry engineered for cost-effective tooling.
Production & Logistics
Heavy-duty mold run and DDP shipping to the USA managed end to end.
Over 50 concepts, one horse-inspired grid
More than 50 grid pattern concepts were explored, drawing on hoof impressions and organic symmetry to give the product a distinct, branded look.
Snap-fit prototypes tested under load
Multiple snap-fit prototypes were built and validated with 3D printing before committing to tooling, to confirm the interlock would hold under vehicle and equipment weight.
Zero-undercut design for cost-effective molding
The geometry was optimized for injection molding with a zero-undercut solution, keeping the mold cost-effective despite the complex interlocking features.
Heavy-duty production and DDP shipping
The mold was engineered for heavy-duty use and validated in its first trial. Large-scale production and container-level logistics, shipped DDP, delivered over 30,000 units to the USA.
What shipped
"A branded, heavy-duty injection molded solution, engineered for the USA market and delivered at container scale."
Questions We Hear About This Project
How do you keep a snap-fit interlock from disengaging under vehicle weight?
Multiple snap-fit prototypes were built and validated with 3D printing under real load before any tooling was committed, so the interlock was proven to hold vehicle and equipment weight before it became a production mold, not after.
Can a branded, aesthetic redesign stay cost-effective to tool at volume?
Yes, by holding a zero-undercut geometry through the redesign. Over 50 grid pattern concepts were explored for the horse-inspired look, but every one was still checked against zero-undercut molding so the branding work never came at the cost of tooling economics.
What gave confidence the production mold would run correctly at 30,000+ units before the first full batch shipped?
The mold was validated in its first trial run before large-scale production began, confirming fill and part quality at the heavy-duty production intent rather than discovering issues partway through a 30,000-unit order.
Have a product to bring to volume production?
Free 30-minute consultation. A real engineer reads your brief, not a bot.