Design for Manufacturing: Why It Can Make or Break Your Product
A CAD model that renders beautifully tells you almost nothing about whether the part can be manufactured. Design for manufacturing, usually shortened to DFM, is the review that closes that gap: checking a design against what the chosen process, material, and volume can actually produce, before a tool is cut or a first batch is ordered.
This guide explains what DFM is, the principles that apply to every process, the specific rules for injection molding, die casting, sheet metal, CNC machining, and 3D printing, and exactly when in product development to run it. It draws on real CADLETE projects, because the clearest way to understand DFM is to see where it saved, or would have saved, a real tool.
What design for manufacturing actually means
Design for manufacturing is the practice of designing a part around how it will actually be made, rather than designing it in isolation and finding out what is wrong once a supplier tries to build it. It looks at the process, the tooling, the material, the tolerance, the finish, and the quantity together, and it asks one question of every feature: can this be produced repeatably, at the target cost, without a compromise nobody signed off on?
You will see two related terms. Design for assembly, DFA, focuses on how the parts come together: fewer parts, fewer fasteners, and an assembly sequence a person or a fixture can actually follow. Design for manufacturing and assembly, DFMA, combines both. In practice a good DFM review always looks at assembly too, because a part that is easy to mold but impossible to fit into its enclosure has not been designed for manufacture at all.
DFM is also not the same as value engineering or cost reduction. Those are done to an existing, working design to take cost out. DFM is done to a design that has not been committed to tooling yet, so that cost never goes in. That timing difference is the whole point.
Seven principles that apply to every process
Whatever the process, the same handful of principles show up in almost every successful DFM review.
- Simplify the part.: Remove features that do not earn their cost. Every extra surface, pocket, or undercut is a place for a defect or an extra tool action.
- Reduce the part count.: Fewer parts means fewer tools, fewer fasteners, fewer assembly steps, and fewer places for tolerances to stack up against each other.
- Keep walls and sections uniform.: Thick-to-thin transitions cause sink, warp, and uneven cooling in molded and cast parts, and uneven stress in formed ones.
- Choose common, available materials.: A material that is easy to source and well understood by your process is cheaper and lower risk than an exotic one chosen for a marginal property.
- Specify tolerances only where they matter.: Tight tolerances everywhere multiply cost and rejection. Tight tolerances on the two mating faces that need them do not.
- Standardize.: Standard fasteners, standard drill and thread sizes, standard cutter radii, and standard sheet thicknesses all avoid special tooling and long lead times.
- Design for the inspection you will actually do.: If a feature cannot be measured on the production floor, it cannot be controlled. Make critical dimensions accessible to the gauge or the probe.
Injection molding: where DFM pays back fastest
Injection molding has the highest tooling cost of the common processes, which is exactly why it rewards DFM the most. A steel production mold is a large, fixed investment, and almost any change after it is cut means machining steel away or welding it back and re-cutting, with a schedule slip measured in weeks.
The core rules are well established. Keep wall thickness as uniform as the design allows, because thick sections sink and thin ones short-shot or cool unevenly. Add draft to every vertical face, commonly in the range of one to two degrees, and more on textured surfaces, so the part releases from the mold without scuffing. Keep ribs thinner than the wall they support, roughly half to sixty percent of the nominal wall, so they do not show as sink marks on the visible face. Round internal corners instead of leaving them sharp, because sharp corners concentrate stress and block flow.
The single most expensive mistake is an undercut: a feature that traps the part in the mold so that it cannot be pulled straight out. Undercuts need side actions, lifters, or collapsible cores, each of which adds tooling cost, maintenance, and risk. Our work on a low-cost air purifier for a USA client was built around eliminating them. A large enclosure meant that every undercut would have inflated the mold cost, so the mechanical design was engineered with zero undercuts from the first concept, which is what kept the injection mold affordable.
Die casting: sculpture versus what a die can release
Die casting forces molten metal into a steel die under pressure, so the rules look similar to injection molding, with the added constraints of metal flow and plating. Sections that are too thin can short-shot before the metal fills them. Sections that are too thick trap gas and shrink. Sharp transitions create hot spots, and detailed sculptural surfaces can plate unevenly unless the geometry is tuned for it.
The Horse-Shaped Handle we developed for a USA premium hardware client is a clean example. The brief was a recognizable horse silhouette in zinc, with a finish that would hold up on a retail shelf. The sculptural surface was reworked in CAD so the die could release it cleanly, with draft angles and wall thickness tuned specifically for zinc die casting. That DFM stage ran before any tooling investment was committed, and the project went from concept to a production batch in twelve weeks with a single production die built.
The lesson generalizes. When a design is as much sculpture as engineering, the DFM review is where the sculpture gets translated into something a die can actually make, without losing what made it distinctive.
Sheet metal: bends, holes, and the rules that crack parts
Sheet metal tooling is cheaper than molding or casting tooling, which tempts teams to skip DFM. It should not, because the failures are different but just as costly: cracked bends, distorted holes, and parts that cannot be formed because a flange is too short to grip.
The commonly used starting points are straightforward. Set the inside bend radius at least equal to the material thickness, and more for harder or thicker material. Keep holes at least two times the material thickness away from an edge, and keep them clear of bend lines, because a hole too close to a bend stretches into an oval. Allow flanges long enough for the tooling to grip, commonly around four times the thickness. Add relief cuts where bends meet so the material does not tear at the corner. These are starting points, not laws, and the right values depend on the material, grade, and the press brake, so confirm them with the manufacturer who will make the part.
Our Barn Hardware Products project for a USA horse barn supply company combined several of these processes: VMC-machined metal components, sheet metal fabrication, and PVD and powder coatings for corrosion resistance. Heavy-duty latches, cane bolts, and handles all had to be designed with the manufacturing sequence in mind, including how each part would be formed, finished, and fitted, before prototypes were approved and full-scale production started.
CNC machining: designing for the cutter, not the render
CNC machining needs no mold, so there is no tooling to rework, but cost is driven by machine time, setups, and tool access. A feature that cannot be reached by a standard cutter needs a special tool, an extra setup, or a different process.
The rules follow from how a cutter works. Internal corners need a radius, because a rotating cutter cannot make a sharp inside corner, and the radius should match a standard tool. Deep, narrow pockets are slow and prone to tool deflection, so keep depth to a sensible multiple of width. Prefer standard hole and thread sizes. Reduce the number of setups by designing features that can be reached from as few sides as possible, because every extra setup adds cost and a small positioning error.
Our Airsoft Gun Housing project shows DFM changing a design rather than just checking it. The housing had been designed for 3D printing, and the goal was to make it fully compatible with CNC machining in aluminum while keeping its strength and look. The design was re-engineered for proper tool paths, tolerances, and manufacturability, machined as prototypes on a VMC to validate fit, and reduced in weight through structural analysis. A 3D-print design and a machinable design are different designs, and treating them as the same file is one of the most common DFM misses.
3D printing: forgiving, but not free of rules
3D printing removes most tooling constraints, which is why it is so useful for prototypes, but it has its own DFM rules. Walls below a process-specific minimum will not print reliably. Overhangs need support or a redesign, and the orientation of the part on the build plate changes strength and surface quality. Trapped powder or resin in sealed cavities has to be able to escape.
The bigger DFM point is that a part that prints well is not automatically a part that molds well. If the end goal is injection molding, designing the prototype with draft, uniform walls, and no undercuts from the start means the move to tooling is a controlled step instead of a redesign. That is the exact transition covered in our guide to moving from 3D printing to injection molding.
DFM checks by process at a glance
| Process | What to check first | Typical failure if skipped |
|---|---|---|
| Injection molding | Uniform walls, draft on every vertical face, no undercuts, rounded internal corners, ribs thinner than the wall | Sink marks, warp, a mold that will not release, side actions that inflate tooling cost |
| Die casting | Wall thickness, draft, smooth section transitions, geometry that plates evenly | Short shots, porosity, trapped gas, uneven plating on detailed surfaces |
| Sheet metal | Bend radius at least the material thickness, holes away from edges and bends, flange length, relief cuts | Cracked bends, oval holes, parts that cannot be formed |
| CNC machining | Standard cutter radii on internal corners, pocket depth, standard holes and threads, number of setups | Special tooling, extra setups, long machine time, deflected features |
| 3D printing | Minimum wall, overhangs and supports, build orientation, escape paths for powder or resin | Failed prints, weak layers, trapped material, a design that cannot move to tooling |
Tolerance and finish: the DFM decisions that quietly set the price
Two specifications drive manufacturing cost more than most designers expect: tolerance and surface finish. Both are easy to write on a drawing and expensive to deliver, and both are frequently over-specified because nobody was asked what the part really needs.
A tolerance should come from function. Ask what the feature has to do: locate a mating part, seal against a gasket, or simply sit inside an envelope. Only the first two usually need tight control, and only on the surfaces that actually mate. Applying one blanket tolerance to the whole part forces the manufacturer to inspect and often reject features that never mattered. Tolerance stacks matter too. When several parts assemble in a chain, small variations add up, so the DFM question is which one or two dimensions to hold tightly so the chain still closes.
Finish deserves the same discipline. A cosmetic surface on a face nobody sees is cost with no benefit. Plating, polishing, and texture also constrain the geometry: a deeply recessed or sharply detailed area plates and polishes unevenly, and texture on a molded part needs extra draft to release. Deciding the finish early, and which faces are cosmetic, lets the design and the tooling be built around it instead of fighting it later.
DFM for electronics, enclosures, and box builds
DFM becomes more valuable, not less, when a product contains electronics. The enclosure is a manufactured part, the PCB is a manufactured part, and they have to fit each other, with room for connectors, heat, cabling, and a person servicing the product later. Reviewing them separately, often at different vendors, is how a board that fits on screen ends up fouling a rib in the housing.
Our low-cost air purifier shows the integrated approach. The mechanical design had to stay free of undercuts for the mold while still fitting a complete PCB system and a display interface within a tight budget, and the user experience work focused specifically on how easily the filter could be replaced. Those are manufacturing, electronics, and usability decisions that only work when they are made together. Our Pickleball Scoring System, which combines PCB design, firmware, and three mounting variants, followed the same logic: the hardware, the enclosure, and the way the unit mounts were reviewed as one product.
For electronics, add three checks to the usual list. Confirm that every connector, button, and light has a clean opening that the enclosure can mold or cut without a fragile feature. Confirm there is a plan for heat, because a sealed enclosure with no airflow path is a design decision, not a detail. And confirm the product can be assembled and, if needed, opened again, because a design that cannot be serviced is expensive to support. This is also why we treat box build assembly as part of DFM rather than a step that happens after it.
Five DFM mistakes we see most often
These come up again and again, across very different products and industries.
- Designing the render, not the process.: A beautiful surface that the chosen process cannot produce is the most common starting point for a failed first article.
- Treating a 3D-print design as a production design.: A part optimized for printing usually needs real changes before it can be molded or machined.
- Over-specifying tolerances and finish.: Blanket tight tolerances and cosmetic finishes on hidden faces add cost without adding value.
- Reviewing the enclosure and the electronics separately.: Parts that fit individually can still clash when they come together, and the clash is found at the worst moment.
- Starting DFM after the tool is ordered.: By then the cheapest fixes are gone and every change is a rework.
When to run DFM: at the start, not at the end
A DFM fix on a CAD file costs an afternoon. The same fix after a production tool has been cut costs a tool rework, a schedule slip measured in weeks, and in the worst case a second tool paid for in full. That asymmetry is why DFM is not a final gate before manufacturing. It has to run as a design constraint from the first CAD model.
In practice there are three natural moments. The first is concept, where a light DFM pass stops you committing to a form that the intended process cannot make. The second is the detailed CAD stage, where the full rule set above is applied feature by feature. The third is before tooling release, where a final formal review confirms that every open point has been closed, including tolerances, finish, material, and the inspection plan.
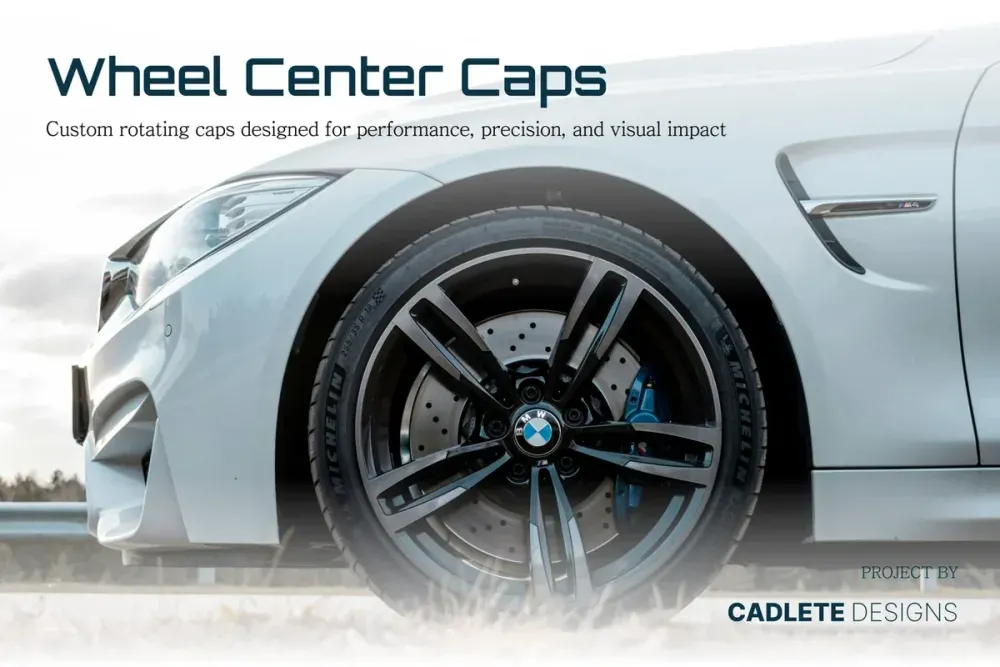
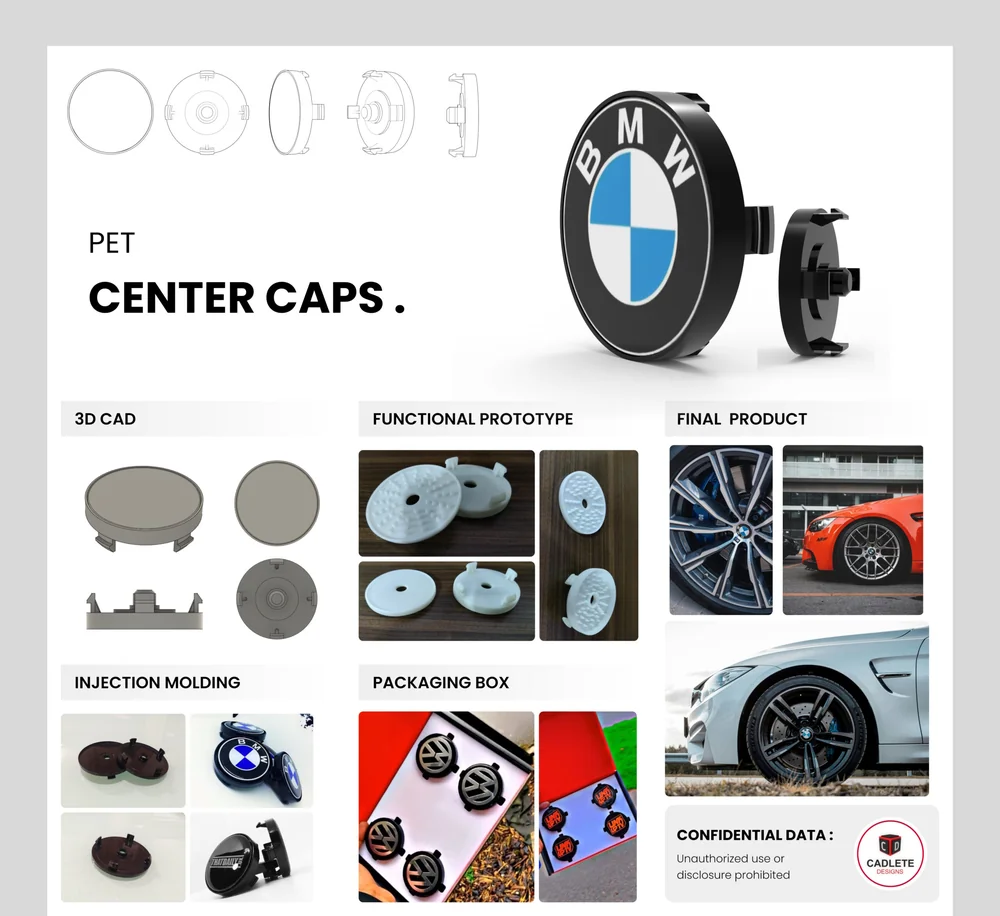
A prototype is the best DFM instrument you have, which is why we like to build prototypes that behave like the production part. On the Rotating Wheel Center Caps project for a UK automotive aftermarket client, SLA prototypes were tested on actual vehicles, not just on a bench, to validate fit and rotation before injection molds were developed across six diameter variants. The tooling decision was made against evidence, not hope.
The real cost of skipping it
The projects that skip DFM are rarely the ones where nobody knew better. They are the ones where design and manufacturing were handled by different teams, or different vendors, with no one whose job was to check the design against the actual tooling before it got expensive.
That is the practical case for keeping design and manufacturing under one process. The person who understands what the mold, the press, or the machine can actually do reviews the part while it is still a CAD file, instead of after the first batch comes back wrong. For a deeper look at how the money actually moves, read our breakdown of the real cost of skipping DFM before tooling.
DFM across markets: drawing standards and expectations
If you design in one country and manufacture in another, part of DFM is making sure the drawing means the same thing on both sides. The most common source of misunderstanding is the tolerancing standard. ASME Y14.5 is the dominant geometric dimensioning and tolerancing standard in the United States, particularly in aerospace and defense, while ISO GPS is more common among companies headquartered in Europe and in many global OEMs. The two overlap heavily but differ in philosophy and details, so state which one your drawing follows.
Units and expectations also vary. US buyers often work in inches and expect a detailed master service agreement with tooling ownership spelled out. European buyers, particularly in Germany, tend to expect documented process discipline and written specification sign-off before tooling. Buyers in the UK and EU also tie DFM to certification readiness, for example CE and RoHS, because a design change late in the process can reopen compliance work. None of this changes the engineering. It changes what has to be written down, and writing it down early is itself a form of DFM.
What each market tends to ask for in a DFM review
| Market | Common drawing standard | What gets scrutinized first |
|---|---|---|
| USA | ASME Y14.5, often in inches | Unit cost at volume, lead time, and tooling ownership stated in writing |
| UK and EU | ISO GPS, in millimeters | Compliance readiness alongside cost, and data and IP handling |
| Germany | ISO GPS, in millimeters | Documented process control and a precise written specification before tooling |
| Canada | ASME Y14.5, inches or millimeters | Country of origin and trade documentation, alongside cost |
| Australia | ISO-based, in millimeters | Total cost of engagement, including communication and time-zone overhead |
| Singapore | ISO-based, in millimeters | Whether the partner can go beyond prototyping into a real first production run |
A practical DFM checklist before you send files
Run through this list before you request a quote or release a tool. Every item you can answer in advance removes a round of questions later.
- Which process and material is this part actually intended for, and at what annual volume?
- Are all walls uniform, and do all vertical faces carry draft where the process needs it?
- Are there any undercuts, and if so, are they necessary and are they costed?
- Which dimensions are critical, and have tolerances been loosened everywhere else?
- Are internal corners, bend radii, and holes set to standard values for the process?
- What is the surface finish or plating requirement, and does the geometry support it?
- Can every critical dimension actually be measured on the production floor?
- Which drawing standard and units does the manufacturer expect?
- How will the part be assembled, and has the assembly sequence been tested on a prototype?
How a DFM review works with us
We run DFM as part of design and manufacturing, not as a separate paid exercise that ends in a report nobody acts on. You send CAD files, and an engineer reviews them against the process you intend to use, flags what will cause trouble, and proposes specific changes with the reason for each. Where a change would alter the look or function, we show the trade-off so the decision stays yours.
Because the same team designs, prototypes, and manufactures, the review is informed by what our own molds, presses, and machines have actually done, not by a generic rulebook. A real engineer reads your brief, a non-disclosure agreement is signed before technical files are shared, and you hear back within twenty-four hours.
Want a DFM review of your part?
Send us your CAD files and the process you have in mind. We will tell you what will cause trouble before a tool is cut, and what it would cost to fix now.
Design for manufacturing FAQ
What is design for manufacturing in simple terms?
It is designing a part so it can be made reliably and at the target cost with the process you have chosen. Instead of finishing the design and then discovering what is hard to make, you check the design against the process, material, and volume while changes are still cheap.
What are the main principles of DFM?
Simplify the part, reduce the part count, keep walls and sections uniform, use common and available materials, specify tight tolerances only where they matter, standardize features and fasteners, and make sure critical dimensions can be measured in production.
What is the difference between DFM and DFMA?
DFM focuses on making each individual part easy to produce. DFA, design for assembly, focuses on how the parts go together. DFMA combines the two, so the whole product is easy to make and easy to assemble.
When in product development should DFM happen?
As early as the first concept, then again at the detailed CAD stage, and once more as a formal review before tooling is released. The earlier a manufacturing problem is found, the cheaper it is to fix.
How much does a DFM review cost?
Cost depends on the number of parts and how complex they are, so there is no flat price. A review done before tooling almost always costs far less than reworking a steel mold afterwards, which is why it is the best-value engineering step in most hardware projects.
Does DFM change how my product looks?
Sometimes slightly, for example adding draft or rounding an internal corner. Good DFM keeps the intent of the design and only changes what the process cannot make, and it shows you the trade-off before anything is changed.
Is DFM only for injection molded parts?
No. DFM applies to every process, including die casting, sheet metal, CNC machining, and 3D printing. Injection molding simply rewards it the most, because its tooling cost is the highest and the hardest to change after the fact.
What is the difference between DFM and value engineering?
Value engineering takes cost out of a design that already works. DFM is applied before tooling is committed, so the cost never goes in. They complement each other, but DFM comes first.


